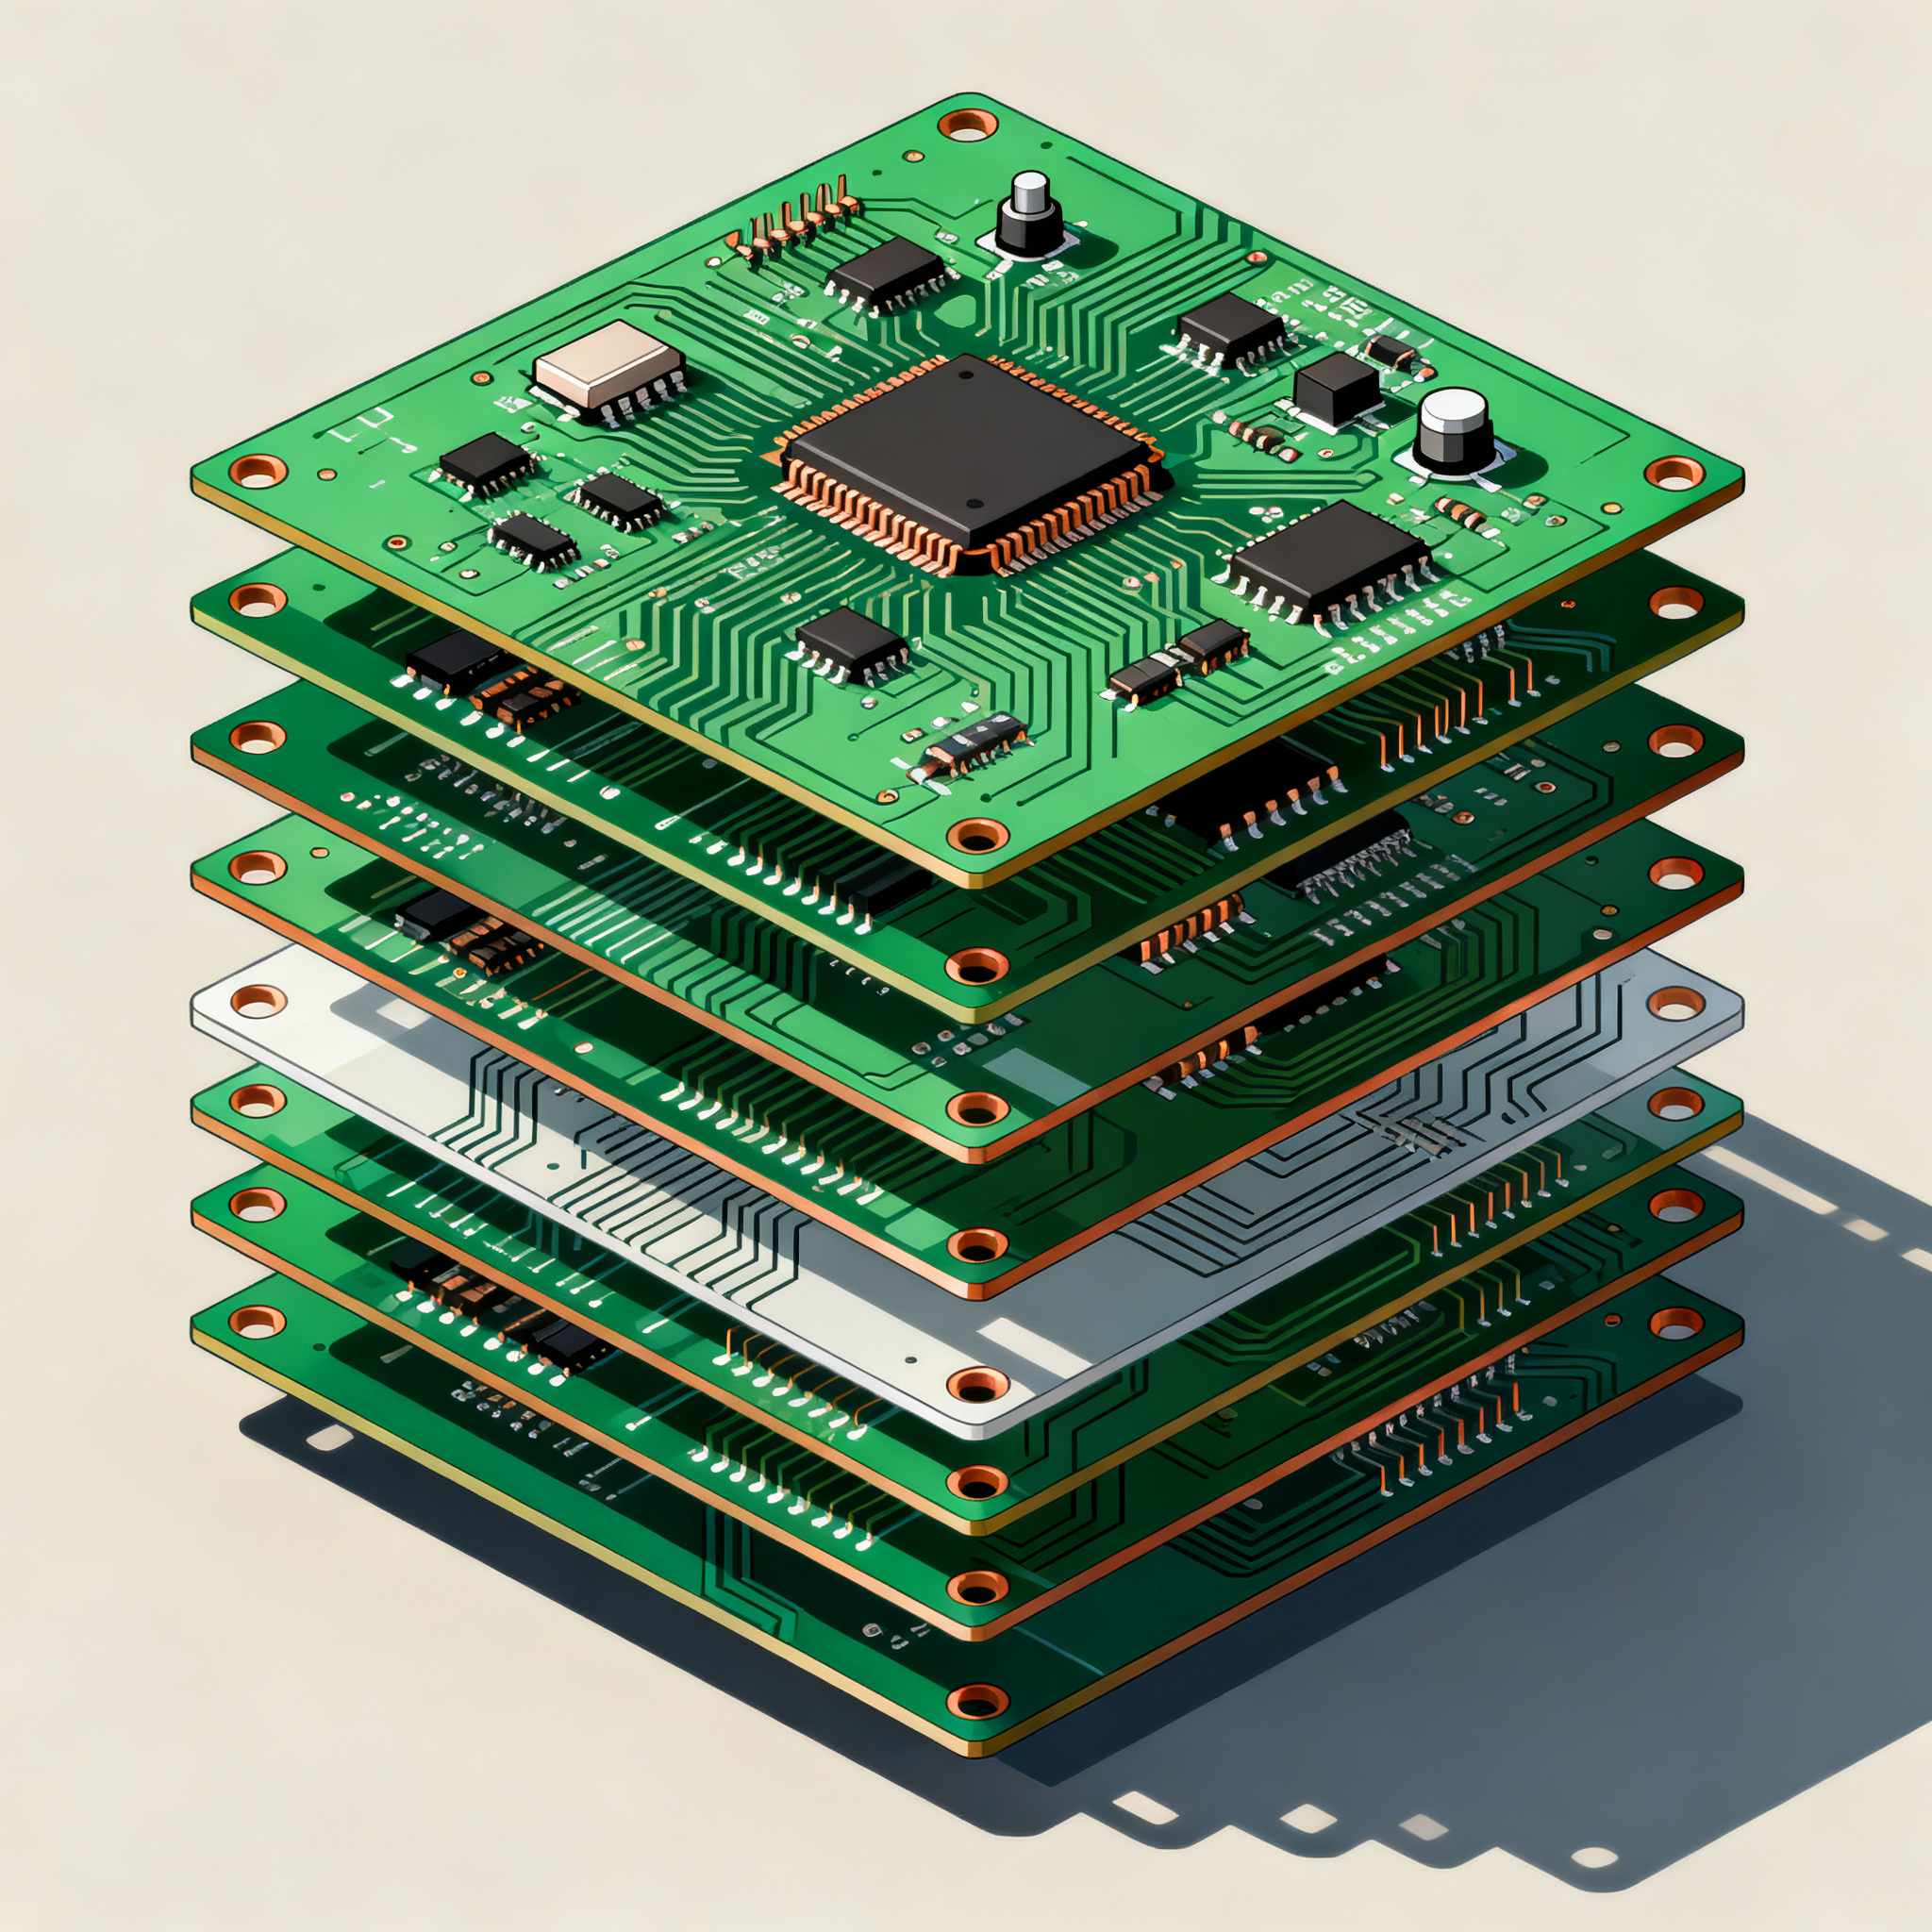
The Signal Integrity Engineer’s Field Guide to 6-Layer PCB Stack-Up Optimization
Why 6-Layer Stackups Now Dominate High-Speed Boards (And Where They Still Fail) You’ve outgrown 4 layers the moment a DDR4 bus, a SerDes link, or a bank of fast ADCs forces a choice between controlled...
Why 6-Layer Stackups Now Dominate High-Speed Boards (And Where They Still Fail)
You’ve outgrown 4 layers the moment a DDR4 bus, a SerDes link, or a bank of fast ADCs forces a choice between controlled-impedance routing and a solid reference plane—on a 4-layer board you can’t have both everywhere. The six-layer board has become the workhorse of high-speed digital and mixed-signal designs, not because it’s exotic, but because it opens a noise floor you simply cannot reach with two signal layers and a single power/ground pair. Yet the step from 4 to 6 layers introduces its own class of failures, many of which surface only after fabrication when a return-path discontinuity turns a clean layout into a compliance-nightmare.
The physics is straightforward but unforgiving. A 4-layer stackup laces return currents through split power planes or forces them to travel across vias to the ground plane on the opposite side, creating loop inductance that eats noise margin at edge rates below 500 ps. Six layers give you at least one tightly coupled plane pair per high-speed signal layer, eliminating the shared-return compromise that plagues 4-layer boards. But that promise evaporates when a design team treats the stackup as a fabrication afterthought. Camptech II Circuits Inc. documents exactly this tension in their pre-release checklist for 6-layer approval, where they require evidence of return-path inspection, power/thermal review, and a locked dielectric stack before a board goes to panel source. Their experience mirrors a pattern we see weekly: a layout that simulates perfectly on paper shows 15–20% overshoot in the lab because the real dielectric constant of the core material didn’t match the library, or because a stitching capacitor was placed at the wrong side of a reference transition.
Stackup-driven signal integrity failures are often misdiagnosed as driver weaknesses or termination mistakes. AllPCB’s primer on managing signal integrity problems catalogues the classic symptoms—eye-diagram collapse, jitter amplification, and non-monotonic edges—and ties them directly to stackup decisions made without a field solver source. Their insight is brutal: “Signal integrity challenges arise as PCB designs push toward higher speeds and denser layouts, affecting data transmission quality across traces and vias.” Six layers are not a shield against that statement; they are the stage on which those challenges either get resolved or turn into expensive re-spins. When a differential pair on an inner layer loses its tightly coupled return because the adjacent plane is a poorly bypassed power pour, the additional layers become the problem, not the solution.
The context, then, is this: the industry has shifted toward 6-layer stackups as the default for any board carrying interfaces above roughly 1 Gbps, but the workflows that guarantee a quiet board haven’t kept pace with the fab economics that made 6 layers cheap. The field guide that follows bridges that gap—it shows you which dielectric spacing tables you can trust, how to compare 4, 6, and 8 layers with actual cost data, and what checks to perform before you release a design that a fabricator will build exactly to your notes, not to your intent.
Inside a 6-Layer Stackup: Return Paths, Dielectric Spacing, and the Thermal Angle
A six-layer board is not a 4-layer design with two extra copper sheets jammed into the middle. It’s a coupled transmission-line structure where every high-speed trace relies on its adjacency to a continuous plane to contain the electromagnetic field. When you define a stackup, you aren’t just choosing a sequence of copper and FR-4; you’re setting the characteristic impedance, the propagation delay, the coupling coefficient to neighboring aggressors, and the thermal bottleneck that will determine whether the board survives a 30-minute burn-in.
The configuration that has proven itself across thousands of DDR3/DDR4, PCIe Gen 3/4, and 10G Ethernet designs is SIG/GND/PWR/SIG/GND/SIG. Signal layers top and bottom sandwich the core; the internal signal layer is buried between a power plane and a ground plane, giving it the lowest loop inductance and best immunity to external noise. EMA Design Automation emphasizes that a 6-layer board allows “more flexibility for routing and better control over signal integrity, making it more appropriate for high-speed applications” with critical signals placed on the top layer source. In practice, that assignment works only if the power plane on Layer 3 overlaps the ground on Layer 5 and all three signal layers can reference at least one solid plane without crossing a moat.
PCBark’s aggregated data sheet, compiled from IPC standards, university signal-integrity research, and industry leader recommendations, provides a sanity check on the numbers engineers actually use source. The typical dielectric thicknesses for a 1.6 mm total stack with 50 Ω single-ended impedance land in the 3.5–4.5 mil range for prepreg between signal and plane, assuming 0.5 oz copper and an effective Dk of about 4.2. The table below summarizes the three most prevalent 6-layer arrangements, the impedance windows they support, and their noise-coupling characteristics. Use it as a starting point, not a locked specification; your fabricator’s final laminate selection will shift Dk and thickness tolerance, and only their impedance modeling guarantees the target.
| Layer Sequence (Top → Bottom) | Typical Dielectric Spacing (Prepreg/Core) | Single-Ended Impedance Window (50 Ω) | Differential Impedance Window (100 Ω) | Return-Path Quality & Notes |
|---|---|---|---|---|
| SIG / GND / PWR / SIG / GND / SIG | Prepreg 3.8 mil (L1-L2), Core 6 mil (L2-L3), Core 28 mil (L3-L4), Prepreg 6 mil (L4-L5), Prepreg 3.8 mil (L5-L6) | 50 Ω ±10% with 5 mil trace | 100 Ω ±10% with 5/5 mil spacing | Every signal layer directly adjacent to continuous ground or power; L4 sandwiched between planes is the quietest. Symmetrical construction minimizes warp. |
| SIG / GND / SIG / PWR / GND / SIG | Prepreg 4.2 mil (L1-L2), Core 5 mil (L2-L3), Core 28 mil (L3-L4), Core 5 mil (L4-L5), Prepreg 4.2 mil (L5-L6) | 50 Ω with 5.5 mil trace | 100 Ω with 6/6 mil spacing | Two signal layers (L1, L3) share GND on L2; L3 returns on PWR on L4 require stitching caps. Good for dual-stripline but demands careful power continuity. |
| SIG / PWR / GND / SIG / GND / SIG | Prepreg 3.5 mil (L1-L2), Core 5 mil (L2-L3), Core 30 mil (L3-L4), Core 5 mil (L4-L5), Prepreg 3.5 mil (L5-L6) | 50 Ω with 4.5 mil trace | 100 Ω with 4.5/5 mil spacing | Top signal returns on PWR plane; requires stitching near connector launch. Slightly thinner prepreg for L1-L2 tightens coupling but reduces voltage breakdown margin on heavy copper. |
AllPCB’s deep-dive into 6-layer secrets reinforces that the numbers only work if you hold copper weight and resin content constant across the panel. Their guide walks through impedance control, material selection, and crosstalk minimization and explicitly warns that swapping a high-resin prepreg for a low-flow variant can shift impedance by 7–10 Ω, enough to violate a ±10% mask source. Thermal performance is equally sensitive: a 0.5 oz internal plane may save weight but raises the junction temperature of a BGA intensely dependent on copper spreading. When you specify a 2 oz power plane on L3, you cut the lateral thermal resistance from 40°C/W to under 20°C/W, a number that directly impacts reliability traces.
Tip: Before finalizing your stackup, run a quick return-path inductance sanity check. For a plane that serves as a reference for signals on two different layers, confirm that stitching vias between ground and power are placed within 20 mils of every signal via transition. The reactive impedance of a 40-mil via loop at 5 GHz can introduce a 3 dB notch that no equalizer can cleanly compensate.
4 vs. 6 vs. 8 Layers: When Two Extra Copper Planes Buy You a Noise Floor
The decision to move from 4 to 6 layers, or from 6 to 8, is rarely about routing capacity alone. It’s about how much noise you can tolerate on a critical receiver before the link budget collapses. The table below compares 4-, 6-, and 8-layer stackups using metrics that drive signal-integrity margins, fabrication cost, and lead time. The data draws on JLCPCB’s direct cost comparison and prototype lead-time figures for 2–32 layers source, their dedicated 6-layer service page with 48-hour turnaround and pricing from $2 source, and Wonderful PCB’s advanced manufacturing and cost analysis source. Use this matrix to anchor trade-off discussions with your procurement team before the schematic has even stabilized.
| Comparison Metric | 4-Layer (SIG/PWR/GND/SIG) | 6-Layer (SIG/GND/PWR/SIG/GND/SIG) | 8-Layer (adds plane pairs) | Selection Criteria & Failure Boundary |
|---|---|---|---|---|
| Typical production cost (100x100 mm, FR-4, 5 pcs) | ~$5–10 (JLCPCB prototype) | ~$15–25 (JLCPCB from $2, 48h delivery option) | ~$35–60 | Choose 4L only if one BGA or all critical buses share a common plane; cost doubles at 6L but buys two critical reference planes. |
| Lead time (standard, no HDI) | 3–5 days | 3–5 days (JLCPCB 2–6 layers most economical) | 5–7 days | Six-layer maintains the same quick-turn tier as 4-layer at major fabs, making it a zero-schedule penalty step. |
| Minimum via aspect ratio (through-hole, 1.6 mm board) | ~10:1 (0.15 mm drill) | ~10:1 (0.15 mm drill) | ~10:1, but laser vias common | Keep drill size ≥0.2 mm if possible; aspect ratio above 8:1 raises plating risk and signal stub issues on thick boards. |
| Crosstalk margin (FEXT) between parallel adjacent traces | Baseline; must share return plane or split planes, increasing coupling | Up to 10–12 dB lower FEXT vs. 4L with proper plane sandwich | Another 4–6 dB improvement when every signal layer has dedicated adjacent planes | Move to 6L if far-end crosstalk on DDR address bus exceeds –25 dB at 1600 MT/s. |
| Impedance control window | ±15% typical; limited by single plane pair coupling | ±10% achievable across all signal layers | ±8% with proper material callouts | If your SerDes requires ±10% on 100 Ω differential, 4L stretches manufacturing tolerances; 6L is safer. |
| Power distribution network (PDN) impedance | High-loop inductance; PWR/GND spacing often >40 mil | Planar capacitance from close PWR/GND pair (4–6 mil) drops PDN impedance below 10 MHz | Multiple plane pairs give ultra-low impedance across a wider band | If your core supply has a sensitive PLL, the 6L’s tight plane pair can eliminate a ferrite bead filter. |
The data shows that 6 layers sit in a sweet spot: they add a second plane pair without crossing into the cost and manufacturing complexity of an 8-layer construction that requires sequential lamination. JLCPCB’s 6-layer prototype offering—starting at just $2 and capable of 48-hour delivery—proves that the economics of 6-layer boards have shifted decisively in the last three years. Wonderful PCB’s analysis further highlights that when you add layers you must also add symmetry to avoid warp, and a 6-layer stackup inherently maintains balance as long as the copper distribution is mirrored about the centerline. The cost increment over 4 layers is now small enough that the signal-integrity margin alone justifies the spend, particularly for any design where compliance testing is not optional.
From Layout to First-Pass Success: Practical Checks That Prevent Re-Spins
You have the stackup locked, the impedance models approved, and the routing nearly complete. The next eight hours of checking will determine whether your first prototype passes eye-diagram mask tests or triggers a frantic three-week debug. I’ve distilled the pre-tapeout routine that experienced signal-integrity engineers, fabricators, and failure-analysis labs converge on. It’s not a substitute for a full simulation workflow, but it catches the stackup-related faults that simulation sometimes misses because the material library didn’t account for the actual glass style.
Blind Buried Circuits’ field guide to signal integrity failures documents the most common root causes after fabrication: impedance mismatches from incorrect stackup assumptions, via stub resonances, and crosstalk due to poor return-path design source. Their list aligns with the checks that Camptech II Circuits recommends before releasing a six-layer board: return-path inspection, power and thermal review, and microvia awareness if the design happens to include them source. Those checks prevent the kind of latent failures that don’t appear in a room-temperature bench test but show up after 100 thermal cycles.
Below is a focused pre-flight checklist specifically for 6-layer boards carrying high-speed traces. Execute each item against the final Gerber and drill files, the approved stackup print, and the post-layout simulation reports. If any item turns red, freeze the tape-out until the root cause is understood.
| Check | Inspection Method | Failure Consequence if Skipped | Acceptance Criteria |
|---|---|---|---|
| Return-path continuity across plane splits | Post-route simulation or visual overlay of signal traces with reference plane polygons | Excessive loop inductance, ringing, and EMI; eye height collapses by 30–40% | No high-speed trace shall cross a reference plane gap; if unavoidable, place stitching capacitor within 50 mils of the crossing |
| Power/ground plane adjacency and decoupling loop area | Impedance analyzer (PDN simulation) and visual check of via placement | Supply ripple couples into signal layers; sensitive PLLs unlock | Smallest decoupling cap loop area; power/ground plane pair spacing ≤6 mils for target-frequency PDN profile |
| Copper balance and symmetry | Calculate percentage of copper on each layer relative to board area; confirm mirror image about center | Board warpage >0.75%, tombstoning on fine-pitch passives, cracked vias under thermal stress | Difference between layers 1/6, 2/5, 3/4 in copper area ≤10%; total asymmetry <5% of board area |
| Impedance coupon placement and trace representation | Verify coupon stackup and trace geometry matches the actual signal layer environment, including same nearby copper pour | Fabricator measures correct coupon but board traces are off by 8 Ω due to local copper density effect | Coupon on same panel, same stackup region, with representative single-ended and differential patterns |
| Signal layer assignment relative to BGA breakout | Check that all high-speed diff pairs from BGA pads are routed only on layers directly adjacent to a continuous ground, not a partial power shape | Return-path interruption right at the launch; near-end crosstalk spikes | Every differential signal shorter than 2000 mils has an uninterrupted reference plane for its entire length |
In addition to the table-driven checks, follow these layout rules—they address the thermal and simulation gaps unique to 6-layer boards:
- Validate the actual Dk and Df of your laminate, not the data-sheet number. Request a TDR measurement from your fabricator’s coupon or use an in-situ ring-resonator structure on a test coupon. AllPCB’s high-speed guide shows that resin-content variation alone can swing Dk by 0.3, which translates to an impedance shift of 5–7 Ω on narrow traces source.
- Run a thermal simulation for the power plane current density. A 1 oz plane carrying 15 A across a 30-mil neck will locally heat above the glass-transition temperature. Use the stackup’s actual copper thickness and multiply by the via field resistance when current changes layers. Camptech II’s review practice emphasizes the need for thermal evidence before approval, particularly when the board includes microvias or heavy copper fill source.
- Check via stub lengths at the highest interface data rate. On a 6-layer board, a through-hole via from top to bottom creates a stub if the signal only travels from layer 1 to layer 2. At 25 Gbps, a 60-mil stub can cause a deep notch in the insertion-loss profile. Backdrill or use blind vias only when the stub length exceeds 15 mils for data rates above 12.5 Gbps.
- Rule-check your fabricator’s stackup before accepting the pre-production panel. Don’t assume the approved stackup survives the translation to CAM. Request a cross-section micrograph of the first article and verify dielectric thicknesses and trace widths match the modeled values within your impedance budget, typically ±10%. Blind Buried Circuits stresses that stackup data errors are a primary cause of field signal-integrity failures source.
Six-Layer Stack-Up Questions Engineers Ask Before Tape-Out
Q: What dielectric spacing typically hits 50 Ω single-ended on a 6-layer board with FR-4?
With a standard SIG/GND pair on a 1.6 mm total thickness, roughly 3.5–4.5 mils of prepreg between the signal layer and its adjacent plane will land near 50 Ω, but the exact value depends on trace width, copper weight, and the resin content of the chosen laminate. Always lock the stackup with your fabricator before routing, using their impedance model.
Q: When do microvias become mandatory, and when can I stay with through-hole vias?
A standard 6-layer board does not inherently require microvias. Through-hole vias are sufficient unless you need to escape fine-pitch BGAs or route blind connections between layer 1–3 without stubs. Camptech II notes that microvia checks only apply if your construction explicitly includes them, making it an economic decision rather than a performance necessity source.
Q: How does a properly designed 6-layer stackup suppress crosstalk compared to a 4-layer board?
The two extra planes provide more direct return paths and can sandwich each high-speed layer between a ground and a power plane, dramatically reducing loop inductance and fringe fields. In practice, a SIG/GND/PWR/SIG/GND/SIG arrangement can cut far-end crosstalk by over 10 dB compared to a 4-layer SIG/PWR/GND/SIG stackup, assuming identical dielectric thicknesses.
Q: Which material grades should I specify for 10–25 Gbps signals on a 6-layer board?
For 10 Gbps and above, low-loss materials such as Isola I-Speed or Nelco N4000-13 bring Df below 0.010 at 10 GHz, while keeping cost manageable. Standard FR-4 may cause excessive insertion loss and eye closure on long traces. AllPCB’s high-speed guide recommends matching the resin system to the data rate to avoid simulation-to-practice mismatches source.
Q: How can I verify my fabricator’s stackup meets my signal integrity targets before accepting the build?
Request a detailed impedance test coupon report and a cross-section micrograph from the same panel. Compare measured trace widths, dielectric thicknesses, and impedance values against your simulation baseline. The Camptech II review practice suggests logging all dielectric constant and thickness numbers against the approved stackup print and rejecting any lot that deviates beyond your ±10% impedance budget source.
References & Further Reading
- PCB Stackup Design: 6-Layer Signal & Thermal Optimization – Camptech II Circuits Inc.
- How to Manage Signal Integrity Issues in a PCB Design – AllPCB
- 6-Layer PCB Stackup Secrets: Optimizing Signal Integrity for High-Speed Designs – AllPCB
- Why PCB Signal Integrity Fails: Common Problems and Practical Solutions – Blind Buried Circuits
- 6 Layer PCB Design Guide: Stackup, Impedance & Vias – PCBark
- PCB Stackup Design Guidelines – EMA Design Automation
- 6-Layer PCBs vs. 4/8-Layer: Cost, Complexity & Optimization – JLCPCB
- 6-Layer PCB Prototype & Stackup – JLCPCB
- 6 Layers PCB Manufacturing: Advanced Stack-up, Design Guidelines, and Cost Analysis – Wonderful PCB
Turning your stackup into a reliable assembly: A validated 6-layer stackup is only half the battle.