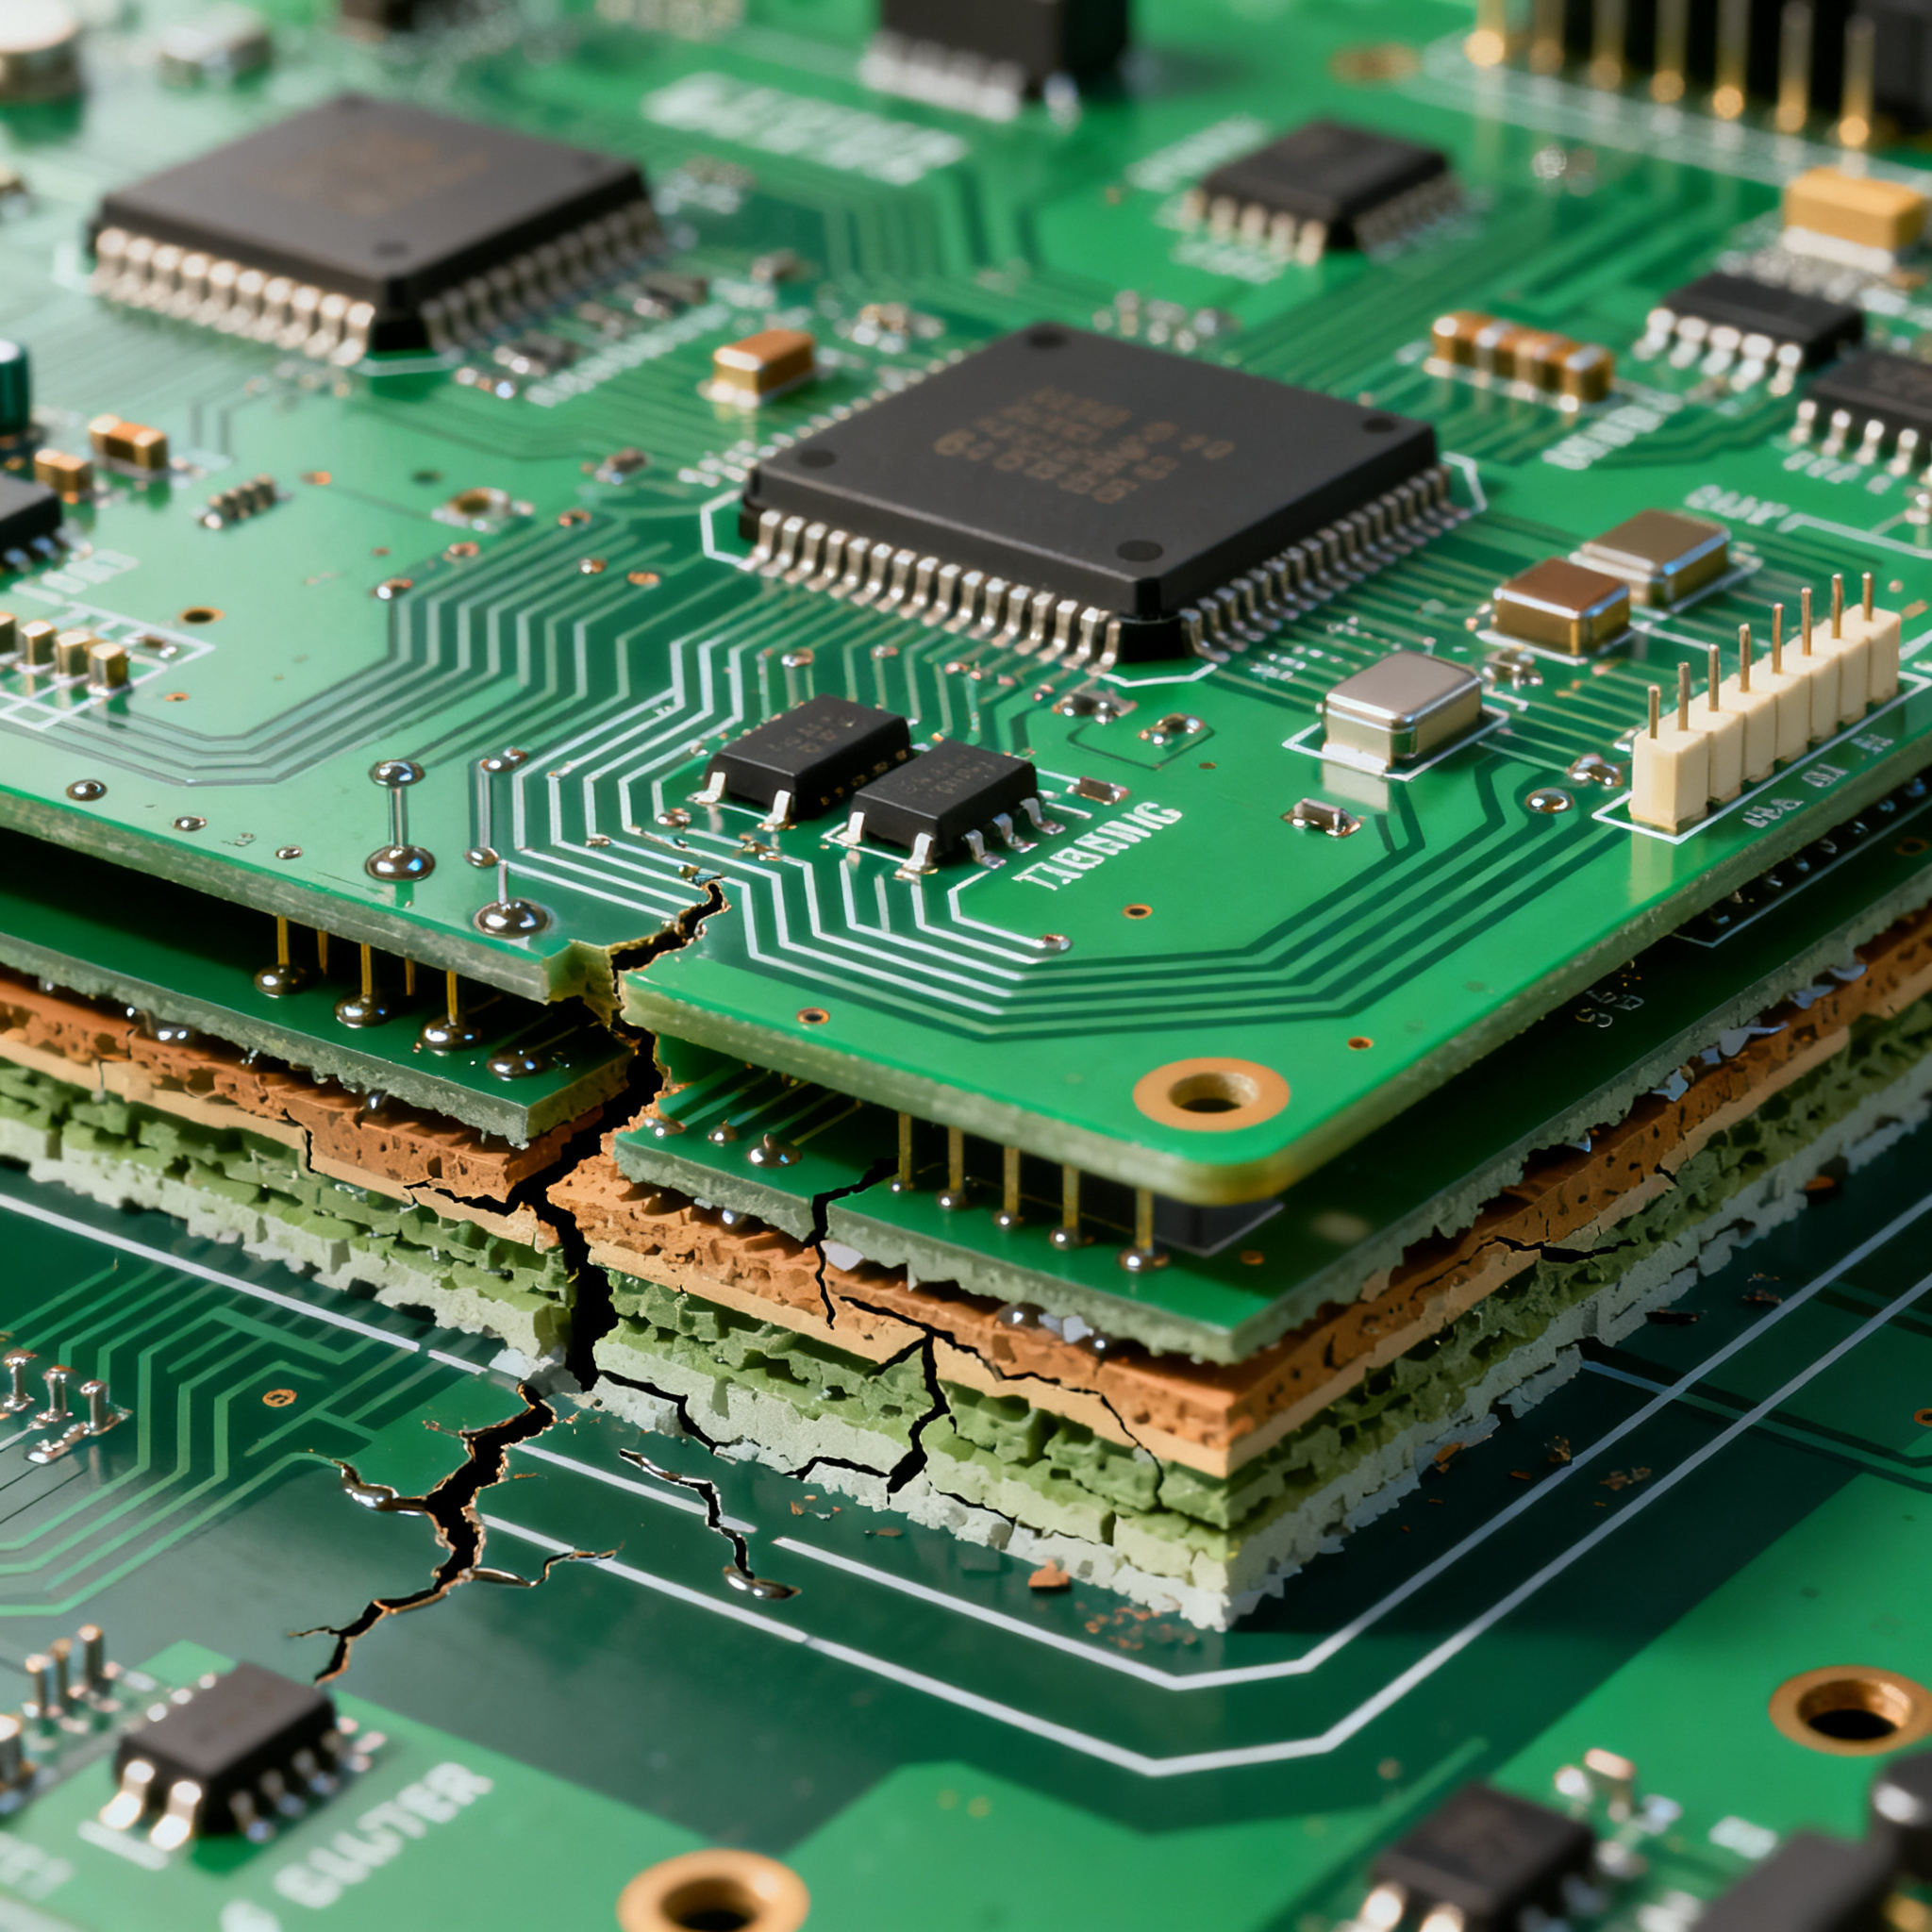
6-Layer PCB Assembly Failure Analysis: Diagnosing Solder Defects, Tombstoning, and Via Failures
When Tombstoning and Via Cracks Stop a 6‑Layer Board in Its Tracks You finish functional test, the board ships, and 90 days later the field return lands on your debug bench with an intermittent open t...
When Tombstoning and Via Cracks Stop a 6‑Layer Board in Its Tracks
You finish functional test, the board ships, and 90 days later the field return lands on your debug bench with an intermittent open that disappears the moment you touch a scope probe. For a 6‑layer PCB assembly, the most elusive failures rarely live on the outer layers. They hide inside a 0.25 mm buried via, under a 0201 capacitor, or along the knee of a plated through‑hole that has been micro‑cracked since the first thermal cycle. At Nova PCBA, engineering teams regularly see 6‑layer assemblies that pass in‑circuit and flying‑probe test yet fail in the field because tombstoned passives lift intermittently and via barrel fractures open when the board reaches operating temperature. These defects sidestep quick visual checks and functional scripts, turning what looks like a mature design into a costly reliability mystery.
The root cause is almost never a single process deviation. A 6‑layer stack‑up concentrates three risk factors that do not appear in simpler 2‑ or 4‑layer designs: asymmetric copper pours that create differential heating during reflow, high‑aspect‑ratio vias that amplify plating stress, and inner‑layer resin starvation that leaves buried via barrels vulnerable to Z‑axis expansion. When a tombstoned 0201 resistor goes unnoticed because the solder fillet still makes mechanical contact at room temperature, or a buried via carries signal only until the board bows under clamp‑down force, the assembly looks healthy on the test floor but degrades over time. That gap between test pass and field life is exactly where failure analysis must start.
IPC‑A‑610 workmanship standards, maintained by IPC, define acceptance limits for solder voids, barrel cracks, and lifted components, but they assume you can see the defect. In a 6‑layer board, many of the worst offenders are invisible without the right combination of X‑ray and cross‑section techniques. The following sections break down the failure mechanisms, compare diagnostic tools, and give you an actionable inspection sequence that catches latent defects before they leave the line.
The Anatomy of 6‑Layer Assembly Failures: Solder Voids, Via Fractures, and Component Uplift
Understanding why a 6‑layer assembly fails differently than a 4‑layer board requires looking at the mechanical and thermal conditions inside the laminate. Three defect categories dominate the failure analysis reports at Nova PCBA: solder voids that originate in the inner‑layer thermal mass, component tombstoning driven by wetting force imbalance, and via barrel fractures caused by coefficient of thermal expansion (CTE) mismatch between copper, glass, and resin.
Solder voids in a 6‑layer board are not simply a paste‑printing issue. The additional copper planes act as heat sinks and gas traps. During reflow, moisture absorbed by the laminate volatilizes and is forced upward through plated through‑holes. If the board reaches liquidus too quickly, the vapor cannot escape before the solder solidifies, creating macro‑voids up to 30% of the joint volume. BGA and QFN packages on a 6‑layer PCB are especially vulnerable because the inner planes delay cooling at the center of the ball array, keeping the solder mobile while outgassing continues. The result is a void distribution skewed toward the inner balls, exactly where 2D X‑ray might miss it if the view angle is not optimized.
Tombstoning of small passives—0201 and 01005 discretes—is exacerbated by the same thermal asymmetry. In a 6‑layer stack‑up, one pad of a component may be connected to a heavy copper ground plane on layer 3, while the other pad connects to a signal trace with minimal copper. During preheat, the pad tied to the plane lags by 5–10°C. The paste on the hotter pad melts first, and the surface tension pulls the component vertical before the second pad wets. Once tombstoned, the open may be intermittent: the component tip can touch the pad when the board flexes, passing functional test, but the joint lacks a proper intermetallic layer and will fail after a few hundred thermal cycles.
Via barrel cracks are the most insidious defect because they are almost always latent. A 6‑layer board often employs buried vias between layers 2–3 and 4–5, with through‑hole vias spanning all six layers. When the board is heated during reflow, the Z‑axis expansion of the laminate can reach 3–5% of the board thickness, while the copper barrel expands less than 1.8%. This delta stresses the plating at the knee of the via, where the inner‑plane pad connects to the barrel. After 20–30 cycles between room temperature and 260°C, micro‑cracks propagate from the resin‑glass interface into the copper, eventually creating an open. The cracks are most common in vias with an aspect ratio greater than 8:1, where the plating thickness at the center of the barrel is thinnest.
The table below maps each defect to its typical root cause, its location within the 6‑layer buildup, and the detection method that consistently reveals it.
| Defect Mode | Primary Root Cause | Typical Location in 6‑Layer Stack | Preferred Detection Method |
|---|---|---|---|
| Solder void (BGA/CSP) | Outgassing trapped by delayed cooling due to inner copper planes | Center balls of BGA, heaviest under large packages on inner‑layer pours | 2D X‑ray with multiple tilt angles; microsection for void location confirmation |
| Solder void (through‑hole) | Moisture in laminate causing blowholes in barrel during wave solder | PTH vias connecting to large plane layers (L2, L5) | X‑ray perpendicular to board; cross‑section of suspect holes |
| Tombstoning (0201/01005) | Unequal wetting due to copper‑pour thermal lag on one pad | Discretes near BGA or adjacent to inner ground plane on layer 3/4 | Post‑reflow optical (angled) + 2D X‑ray for hidden joints; microsection for intermetallic verification |
| Via barrel crack (thermal stress) | CTE mismatch between resin and copper; high aspect ratio (>8:1) | Through‑hole and blind vias crossing resin‑rich regions between L2–L3 or L4–L5 | Microsection with copper‑etch highlighting; thermal shock coupon evaluation |
| Buried via micro‑void | Incomplete resin fill during lamination causing plating voids | Buried vias between layers 2–3 and 4–5 in sequential lamination builds | Cross‑section parallel to via axis; SEM imaging |
| Inter‑plane delamination | Overheating during reflow on poorly bonded prepregs | Between plane layer 3 and dielectric core, near large copper pours | Scanning acoustic microscopy (SAM); cross‑section for gap measurement |
To decide whether a specific void or crack is acceptable, IPC‑A‑610 defines clear boundaries. For BGA and CSP solder joints inspected at Class 2, the total void area shall not exceed 25% of the ball interface area, and no single void may occupy more than 20%. For through‑hole solder fillets, the allowable void percentage is also 25% of the total fillet area. Via barrel cracks are considered a defect when the crack extends more than 25% through the barrel wall thickness or when it reaches a corner that connects an inner‑plane pad. Numerous 6‑layer assemblies that pass initial electrical test are, in fact, non‑conforming under these standards—the cracks and voids are simply too small to detect without the appropriate analytical method. That reality makes the choice of inspection tool the single most important decision in a failure analysis workflow.
X‑Ray, Cross‑Section, or Acoustic Microscopy: Picking the Right Tool to Expose the Root Cause
A 6‑layer PCB hides the failure signature across depth, material, and angle. No single inspection technique gives you the whole picture, so the engineer must select and sequence the tools based on the defect symptom. The three core methods for 6‑layer assembly failure analysis are 2D/3D X‑ray inspection, microsectioning, and scanning acoustic microscopy (SAM). Each targets a different set of anomalies and imposes its own constraints on cycle time and board usability.
2D X‑ray is the workhorse for solder voids, head‑in‑pillow BGA joints, and tombstoned components. When you tilt the detector to 60‑70°, you can see under the BGA ball and catch voids that are offset from the ball center. However, X‑ray cannot distinguish a vertical via crack from normal copper‑plane overlap. It also struggles with buried vias that reside entirely between layers 2–3, where the X‑ray image is a projection of multiple copper features. If your symptom is an intermittent open that correlates with flexure, X‑ray may show nothing useful, and you need to move directly to microsectioning.
Microsectioning—cutting, potting, grinding, and polishing a cross‑section through the suspect region—is the gold standard for via integrity, plating thickness measurement, inner‑layer delamination, and intermetallic compound analysis. It is destructive: that board will never run again. But for a field return or a first‑off proto, the information return is worth the sacrifice. Microsectioning reveals barrel cracks as fine as 2 µm, nailheading from poor drilling, and resin recession at the via knee. Paired with SEM, it can determine whether a crack originated from thermal stress (smooth, conchoidal fracture surface) or from a drilling defect (jagged, glass‑fiber‑smeared walls with debris).
Scanning acoustic microscopy brings the unique ability to detect internal delamination without cutting the board. SAM pulses ultrasound into the part and measures the reflection at material interfaces. Popcorn‑type delamination under large BGAs or within the laminate layers appears as white spots in the acoustic image. For a 6‑layer assembly that overheated during reflow, SAM can pinpoint air gaps between layers 2 and 3 that would be invisible on X‑ray and costly to find through random cross‑sectioning. The trade‑off is that SAM requires immersion in a coupling medium (usually water) and is not suitable for boards populated with unsealed MEMS or open‑cavity packages.
| Metric | 2D/3D X‑ray | Microsectioning | Scanning Acoustic Microscopy |
|---|---|---|---|
| Depth of insight | 3D void distribution, solder joint geometry; limited for vertical cracks | Cross‑section profile: plating thickness, crack path, resin‑glass interface | Internal gaps and delamination at any depth; no volumetric solder data |
| Destructive? | Non‑destructive; board remains functional | Destructive; entire board or targeted coupon destroyed | Non‑destructive if part is compatibility; requires immersion |
| Inline integration | Possible: high‑speed in‑line AXI for BGA and void screening | Off‑line laboratory; 1–3 hours per target | Off‑line; 10–30 minutes per scan, batch possible |
| Relative cost per analysis | Low–medium (equipment amortized over volume) | Medium–high (lab time + skilled technician) | Medium (equipment cost; destructiveness added if board cannot be wetted) |
| Best for | Verifying BGA/QFN voids, tombstoning, head‑in‑pillow; initial screening of field returns | Confirming via barrel cracks, inner‑layer separation, intermetallic thickness, plating anomalies | Detecting popcorn delamination, pre‑reflow laminate integrity, large‑area scanning before microsection |
Engineers who routinely diagnose 6‑layer assembly failures rarely rely on one tool alone. A typical sequence for a via‑related intermittent open might start with X‑ray to rule out obvious solder shorts and gross voiding, then move to SAM if delamination is suspected, and finally target the precise location with microsectioning. The aim is to limit true destructiveness to the smallest possible area while maximizing the information needed to correct the process or the design.
Diagnostic Steps to Catch Tombstoning and Via Failures Before They Escape the Line
Latent defects on 6‑layer boards are preventable if the inspection workflow is designed around the stack‑up, not just the component placement. The following steps, adapted from the process qualification practices at Nova PCBA, form a practical pre‑ and post‑reflow sequence that targets the high‑risk areas specific to 6‑layer assemblies.
- Equalize solder paste deposits on all 0201/01005 pads. Use an SPI (solder paste inspection) system capable of 20 µm height resolution. Adjust stencil aperture dimensions so the paste volume on each pad of a passive component differs by less than 8%. Even a small imbalance can tip the wetting force ratio toward tombstoning when one pad is attached to a heavy inner copper plane.
- Perform first‑off X‑ray sampling on internal layer connections. After reflow, X‑ray at least three fully populated boards at 0°, 45°, and 70° tilt. Focus on BGA corners and any via fields that connect layers 2–3 or 4–5. Look for irregular void patterns that align with resin‑rich regions, not just the ball‑level void percentage.
- Build thermal shock coupons into the panel frame. The coupon should contain representative through‑hole and buried vias with the same aspect ratio as the production board. Subject the coupon to 500 cycles between -40°C and +125°C, then microsection to evaluate barrel crack propagation. This data gives you an early warning before a field failure.
- Correlate via design with IPC‑2221. Keep plated through‑hole and blind via aspect ratios below 8:1. For buried vias where sequential lamination is used, reduce the target to 6:1. Use the IPC‑2221 design guidelines to verify that annular ring dimensions and anti‑pad clearances do not thin the copper barrel at the inner‑plane junction—a frequent crack initiation point.
An equally critical factor is copper balance. Asymmetric copper weight between the top and bottom halves of the 6‑layer buildup creates a bending moment during reflow. The board bows, and the corner BGA balls or QFP leads momentarily lift from the paste before solidification, producing head‑in‑pillow defects or open fillets that can later tombstone under vibration. The table below provides the process parameters we monitor to keep these risks in check.
| Parameter | Target / Limit | Measurement Method | Risk if Out of Limit |
|---|---|---|---|
| Via aspect ratio (through‑hole) | ≤ 8:1; ≤ 6:1 for buried vias | Design rule check; microsection verification | Plating thinning, barrel crack after thermal cycling |
| 0201 pad paste volume balance | ±8% difference per pad pair | SPI with 20µm height resolution | Tombstoning, open fillet |
| Copper symmetry (top vs. bottom half) | ≤ 15% difference in total copper weight per half | Stack‑up weight calculation from Gerber analysis | Warpage >0.5%, head‑in‑pillow, corner opens |
| Reflow ramp rate (soak to peak) | 1.5–2.0°C/s | Profiling with internal thermocouples at board center and edge | Thermal gradient across 0201 pads, tombstoning |
| Time above liquidus (217°C) | 50–75 s for 6‑layer heavy‑copper boards | Reflow profile log, edge vs. center thermocouple | Excessive via stress, delamination |
| Peak package temperature | 240–245°C for standard SAC305 | Thermocouple on BGA package top | Popcorn delamination in large BGAs |
Implementing these checks as a standard first‑off protocol, rather than waiting for a failure, shifts the investment from failure analysis time to defect prevention. For 6‑layer production volumes as low as 200 units, the cost of one field‑return investigation dwarfs the combined effort of SPI, X‑ray sampling, and coupon cycling.
FAQs for the Engineer Tracing a 6‑Layer Assembly Defect
Q: Why does tombstoning occur more frequently on 6‑layer boards with small passives?
Tombstoning is driven by differential wetting forces during reflow. On 6‑layer boards, uneven copper fills and thermal mass in inner planes can create temperature gradients across a component's pads. If one pad heats faster because it connects to a thin signal trace while the other is sunk into a solid copper plane on layer 3 or 4, the solder paste on the hotter pad reaches liquidus earlier, pulling the component upright before the second pad wets. This effect is amplified when 0201 or 01005 parts are placed close to high‑copper‑pour areas, often within 1 mm of a plane edge. A symmetric layout with thermal relief ties on all layer connections reduces the gradient and the tombstoning rate.
Q: How can I distinguish a via barrel crack caused by thermal stress from a drilling defect?
Thermal stress cracks typically appear as vertical fractures in the barrel wall, often accompanied by resin recession at the knee of the via where the inner‑plane pad joins the barrel. They cluster in regions with high glass transition temperature (Tg) mismatch between the resin and the copper, and they usually originate on the inner surface of the hole. Drilling defects, in contrast, show rough or glass‑fiber‑smeared barrel walls, nailheading (flared copper at the via edge), or debris trapped at the inner‑layer junction. Cross‑section analysis followed by SEM imaging reveals the fracture surface: thermal fatigue cracks have a smooth, faceted appearance, while drilling‑induced cracks interrupt jagged glass‑fiber bundles. Correlating the failure location with the layer stack‑up and the aspect ratio helps confirm the mechanism.
Q: What IPC‑A‑610 class 2 acceptance criteria apply to solder voids in 6‑layer through‑hole and BGA joints?
According to the IPC‑A‑610 Class 2 requirements, through‑hole solder joints are evaluated via X‑ray and must exhibit no more than 25% void area in the solder fillet. For BGA and CSP joints, the total void area across the ball interface must not exceed 25%, and any single void must be smaller than 20% of the ball interface area. For high‑reliability designs that push toward Class 3, many assemblers tighten the spec to 15% total and 10% single void. In 6‑layer boards, these limits are challenged by outgassing from inner layers, so meeting Class 2 consistently requires controlling laminate moisture and reflow soak profiles.
Q: How does imbalanced copper distribution in a 6‑layer stack cause warpage and subsequent solder joint failures?
Asymmetric copper weights between the upper and lower halves of the stack create a differential CTE response during heating. If the top three layers contain 35 µm copper each and the bottom three contain only 18 µm, the top expands more, causing the board to bow upward at reflow temperatures. That bow lifts component leads from the paste before solidification, creating head‑in‑pillow BGA joints, open fillets on QFP leads, or tombstoned passives near the board edge. Design for manufacture rules in IPC‑2221 call for copper symmetry within 15% of total weight per half to keep warpage below 0.5%. Verifying symmetry at the Gerber stage prevents a failure that no amount of reflow tuning can fully resolve.
Q: When should I use cross‑section analysis instead of 2D X‑ray to find the root cause of an open via?
Use cross‑sectioning when 2D X‑ray cannot confirm a vertical crack or when the open is suspected inside the barrel wall rather than at the pad connection. A microsection reveals plating thickness profiles, corner cracks, resin shrinkage, and inner‑layer separation—information that X‑ray, even with 3D reconstruction, cannot provide because copper planes obscure the depth. This is the definitive method for verifying buried via integrity in 6‑layer boards where the via is not optically accessible and where the failure may only manifest under thermal or mechanical load. It is also the required step to differentiate a thermal fatigue crack from a manufacturing defect.
References & Further Reading
- IPC — Association Connecting Electronics Industries — IPC‑A‑610 and IPC‑2221 standards for solder joint acceptance and PCB design.
- Nova PCBA — Professional PCB assembly and failure analysis services, with extensive experience in 6‑layer and multi‑layer boards.
- EE Times — Electronics industry publication with in‑depth reliability and manufacturing articles.
- Octopart — Component database and parametric search for verifying component specifications.
- IPC‑A‑610 Acceptability of Electronic Assemblies — The primary workmanship standard referenced for void and crack limits.
- IPC‑2221 Generic Standard on Printed Board Design — Design guidelines for via aspect ratio, copper balance, and stack‑up symmetry.